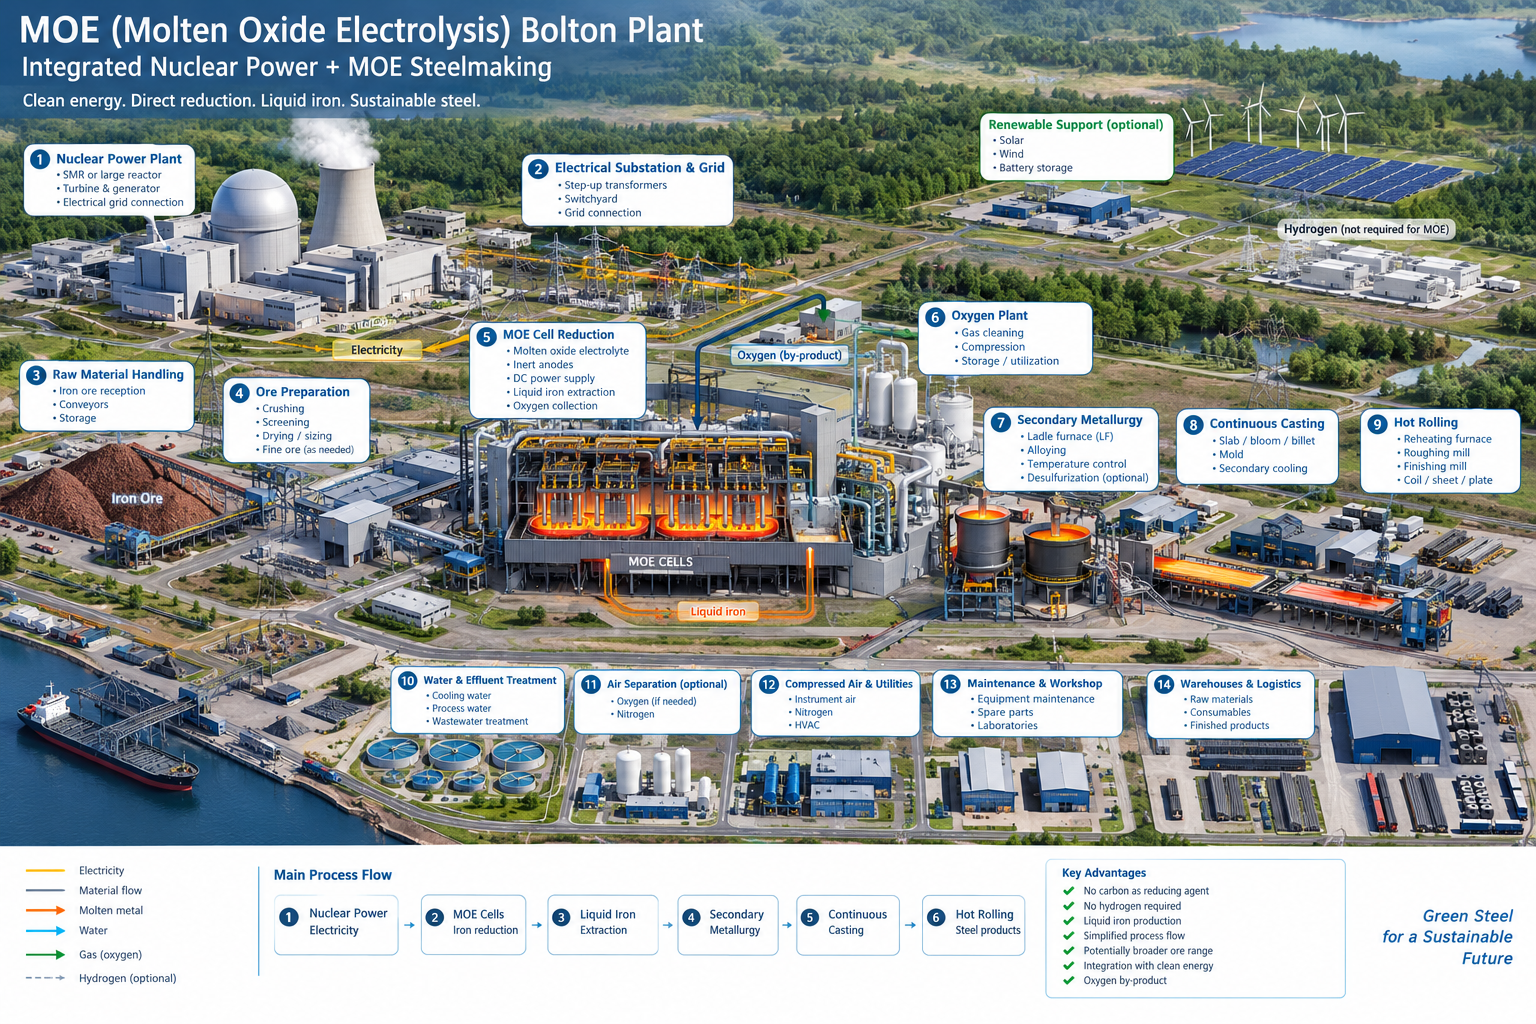
Fig nº 1. Scheme of a future integrated Iron and Steel plant ; MOE Bolton Plant plus Nuclear Power. I.Ibarrondo and AI.
TECHNICAL REPORT
Molten Oxide Electrolysis (MOE) for Steel Production: Current Status, Prospects and Future of the Technology.
October 2026
Ignacio Ibarrondo Martinez – Iturralde
Dr. Ing. Industrial
Formerly Catedrático E.U. (University Basque Country UPV/EHU).
www.ironandsteelmaking.com
https://www.researchgate.net/profile/Ignacio-Ibarrondo/stats
Molten Oxide Electrolysis (MOE) is one of the most radical technologies currently being developed to decarbonize primary iron and steel production. Unlike the conventional blast furnace–LD/BOF route and the emerging H₂-DRI–EAF route, MOE attempts to reduce iron oxide using electricity directly, without using coal, coke, natural gas, or hydrogen as a reducing agent.
The ideal overall reaction can be represented in simplified form as:
Fe₂O₃(l) + 3e⁻ → 2Fe(l) + 3/2O₂(g)
In reality, the electrochemical process takes place through different iron and oxygen species in a molten-oxide electrolyte. The desired result is liquid iron directly in the cell, with oxygen as a by-product, eliminating carbon from the reduction process. MIT demonstrated the concept experimentally (1, 2), and Boston Metal subsequently developed an industrial platform based on MOE (3, 4, 5, 6).
The situation in 2026 is particularly interesting. Boston Metal announced in March 2025 the commissioning of an industrial MOE cell with multiple inert anodes that produced steel at tonnage scale. However, the company subsequently modified its commercial priorities: in May 2026 it raised an additional $75 million and is concentrating its immediate MOE expansion on critical metals, while MOE Steel remains an application for the coming years (4, 5 ).
Therefore :
MOE is not yet a mature commercial technology capable of replacing H₂-DRI on a large scale, but it could become one of the most disruptive technologies in steelmaking in the late 2030s and during the 2040s.
In that case, it would become the third generation of steel production in History: the first being the blast furnace, the second being direct reduction—whether through conventional processes or hydrogen-based reduction—and, finally, the third generation: the Molten Oxide Electrolysis (MOE) Bolton Process.
Index :
Summary pp. 2
- What is Molten Oxide Electrolysis? pp. 5
2.- Physical and chemical fundamentals pp. 7
2.1. The basic electrochemical reaction
2.2 .- Thermodynamics Requirements
2.3 .-The importance of inert anode in the process
2.4.- Operating temperature
3.- Iron and steelmaking process pp . 13
4.-Energy consumption, production volume and process efficiency. pp.15
4.1. Theoretical and real energy requirements in the production process.
4.2. Specific electricity consumption: kWh per tonne of iron
4.3.- The Fundamental Difference MOE Compared with BF and H₂-DRI
4.4.- Potential advantages of MOE over BF and H2-DRI
5.- Industrial development and commercial status pp. 23
5.1.- The Decisive Breakthrough: Boston Metal
5.2.- The Real Situation of the Technology in 2026
5.3.- . News Item That Must Be Correctly Interpreted (2026).
6.-. Main technical challenges and engineering risks pp.27
6.1.- Anode durability and corrosion
6.2.- Electrolyte composition and control
6.3.- Refractory and thermal management
6.4.- Feedstock impurities and steel quality
6.5.- Electrical infrastructure and plant integration
6.6.-. MOE has an Enormous Electricity Requirement
6.6.1.- MOE + Renewables
6.6.2.- MOE + Nuclear Energy: A Particularly Interesting Combination
7.- Extraordinary Advantage: No Hydrogen Required pp.37
8.- MOE Challenges pp. 38
8.1.- MOE Production challenges in relation to BF and DR
8.2.- The Real Challenge: Electricity Cost
8.3.-. Second Major Challenge: Materials
8.4.- Third Challenge: Productivity
8.5.- Fourth Challenge: Electrolyte Control
8.6.-. Fifth Challenge: Impurities
9.- The Iron Produced by MOE pp.43
10.- MOE Compared with the Main Green-Steel Technologies pp.44
11.- Recent lower-temperature MOE research pp.46
12.- Technology Forecast pp.51
13.- Bibliographic references. pp.55
—————-
-
What is Molten Oxide Electrolysis?
MOE is a high-temperature electrometallurgical technology (3, 4, 5, 6, 7, 8, 9), emerging technology for producing primary iron directly from iron oxide by electrochemical reduction. It offers a potential alternative to conventional blast furnace–basic oxygen furnace (BF–BOF) steelmaking and to hydrogen-based direct reduction of iron (H₂-DRI), o conventional DR processes.
The technology most closely associated with industrial development of MOE for steel production is that of Boston Metal. Its process uses a high-temperature electrochemical cell in which iron oxides are dissolved in a molten oxide electrolyte. An electric current reduces iron ions to metallic iron at the cathode, while oxygen is released at an inert anode.
The principal attraction is that the oxygen removed from iron oxide can be produced as oxygen gas rather than as carbon dioxide, provided that the process avoids carbon-based reducing agents and the electricity and auxiliary heat are sufficiently low-carbon. Unlike H₂-DRI, MOE does not require hydrogen production, hydrogen storage or a hydrogen-recycle circuit.
And more, iron and steel production is one of the major industrial sources of greenhouse-gas emissions. Conventional integrated steelworks depend heavily on coal-derived coke, which acts both as a reducing agent and as a source of energy in the blast furnace. Carbon monoxide reduces iron oxides, and carbon dioxide is generated as part of the process.
MOE proposes a fundamentally different approach: using electricity to separate oxygen from iron oxide directly, producing liquid iron without the need for coke, carbon, conventional gas or H2 as a chemical reducing agent.
However, MOE should not yet be treated as a fully proven, commercially mature replacement for conventional ironmaking. Important challenges include inert-anode durability, cell materials, electrical efficiency, electrolyte chemistry, impurity control, continuous operation, scale-up and the cost of electricity.
In summary :
Blast Furnace
Fe₂O₃ + C → Fe + CO and CO₂
or hydrogen:
H₂– DRI
Fe₂O₃ + 3H₂ → 2Fe + 3H₂O
MOE uses electricity:
MOE
FeₓOᵧ + n e–→ Fe + O₂
2.- Physical and chemical fundamentals
NOTE : What is presented here is a highly simplified summary of the physicochemical fundamentals. For a more comprehensive discussion, the reader is referred to the specific bibliographic references provided at the end of the bibliographic section.
2.1. The basic electrochemical reaction
The objective is to decompose iron oxide into metallic iron and oxygen using electricity (8,9 ).
For hematite, the overall idealized reaction is:
Fe2O3(l)→2 Fe(l)+3/2 O2(g)
This is a useful overall representation of the process. In an actual MOE cell, the iron oxide participates in the chemistry of the molten electrolyte, and the electrode reactions occur through dissolved ionic species.
The corresponding simplified cathodic (Pole -) reaction is:
2 Fe3+ + 6 e− → 2 Fe (l)
The anodic (Pole +) reaction can be written as:
3 O2− → 3/2 O2 (g) + 6 e−
The electrons travel through the external electrical circuit, while ionic species carry charge through the electrolyte. The net chemical reaction produces liquid iron and oxygen gas.
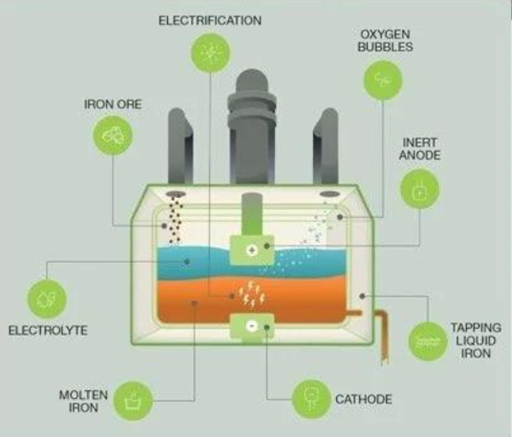
The cell contains:
- iron ore;
- molten-oxide electrolyte; A mixture of molten oxides that allows ionic species to be transported and maintains suitable operating conditions
- cathode; The reduction occurs at the cathode
- inert anodes; The anode must allow
O²⁻ → 1/2 O₂ + 2e⁻
- high-current DC electrical system;
- ore-feeding system;
- liquid-iron extraction system;
- oxygen extraction system.
The iron produced can leave the cell in the liquid state, which is one of the most important characteristics of MOE.
2.2 .- Thermodynamics Requirements
Iron oxide reduction is energetically demanding because the process reverses the formation of a stable metal oxide. The minimum reversible electrical work is related to the Gibbs free-energy change of the overall reaction:
ΔG = ΔH−TΔS
For a reversible electrochemical cell, the minimum decomposition voltage is:
Erev=ΔG/nF
where:
- ΔG is the Gibbs free-energy change per mole of reaction
- n is the number of electrons transferred per mole of reaction as written.
- F is the Faraday constant, approximately 96,485 C mol−1.
- Erev is the reversible decomposition voltage under the specified conditions.
- The real cell voltage must generally exceed the reversible voltage because of electrical resistance, electrode over potentials, concentration gradients, current distribution and other losses.
High operating temperatures can improve reaction kinetics and allow the product iron to remain liquid. However, they impose severe requirements on cell insulation, refractory materials, electrode stability and thermal management
2.3 .-The importance of inert anode in the process
The anode is one of the most important components of the Boston Metal approach.
If a carbon anode is used, oxygen from the oxide can react with the carbon, producing carbon monoxide or carbon dioxide. This undermines the objective of avoiding process-carbon emissions.
An inert or sufficiently durable oxygen-evolving anode must therefore withstand:
–Temperatures around or above the melting point of iron.
–Iron ore is introduced into a molten-oxide electrolyte, maintained at temperatures of approximately 1,600 °C or higher.
–Boston Metal currently describes its MOE Steel cell as operating at approximately 1,600 °C.
–Oxidizing conditions at the electrode–electrolyte interface.
–Corrosion by the molten oxide electrolyte.
–Thermal cycling and mechanical stresses.
–Long periods of operation at high current density.
Allanore, Yin and Sadoway (1) demonstrated a chromium-based alloy approach in which a protective, electrically conductive oxide layer contributes to anode stability. This authors established an important scientific basis for further development, although laboratory stability does not automatically guarantee industrial service life.
Boston Metal identifies its metallic inert anode technology as a critical part of its industrial platform and a technology it intends to supply alongside MOE licensing (13).
2.4.- Operating temperature
Boston Metal describes its MOE Steel process as operating at approximately 1,600 º C. This is above iron’s melting point, approximately 1,538 ºC, enabling liquid-iron production ( 2 ).
The temperature is a defining feature of the commercial concept. It facilitates rapid electrochemical processing and liquid-metal separation, but also makes the selection of anode materials, refractories, electrolyte chemistry and cell architecture exceptionally demanding.
Not every MOE research configuration operates at the same temperature. Lower-temperature experimental systems are in study.
3.- Iron and steelmaking process
The figure nº 1 describes the general sequences of industrial process (2, 4).
- Raw material handling.
- Iron ore preparation.
Iron-bearing feed is selected, characterized and prepared to meet the cell’s chemical and physical requirements. Ore impurities must be accounted for.
-
MOE Cell Reduction ( see Thermodynamics Requirements )
- Molten oxide electrolysis cell.
The feed dissolves or reacts in a molten oxide electrolyte. A high-current DC power supply drives the electrochemical reactions.
- Electrochemical separation
Iron ions are reduced at the cathode, while oxide ions release oxygen at the anode. The liquid metal collects within the cell.
- Secondary Metallurgy Ladle furnace; Alloying and Temperature control .
- Continous casting and / or Strip Casting Technology (11)
- Hot rolling
- Cold rolling
Other Elements:
-
Nuclear Power plant
: SMR or large reactor
This is of crucial importance, as electrical energy is the foundation of this process, and its price and availability will determine whether or not it is implemented on an industrial scale (12).
Electrical Substation
Oxygen plant
Water & Effluents Treatment
Maintenance, Logistic etc….
As I have previously noted, the principal advantage of this arrangement is the potential integration of iron extraction and production of liquid metal in one electrochemical unit, avoiding the separate coke-making, sintering or pelletizing, blast-furnace reduction and basic oxygen furnace stages associated with the conventional integrated route, or shaft furnace and hydrogen production in H2 – DR as new process.
-
Energy consumption, production volume and process efficiency.
4.1. Theoretical and real energy requirements in the production process.
Production volume in t/h at an industrial scale, the electricity consumption of MOE (and its price (12) ) is the decisive factors in its industrial competitiveness. It depends on the thermodynamic requirements, cell voltage, current efficiency, thermal losses and the energy needed by auxiliary equipment.
Faraday’s law relates the amount of iron produced to the electrical charge passed through the cell:
mFe=MFe. I.t.ηF / 3F
where MFe is the molar mass of iron, I is current intensity , t is time, and ηF is the Faradaic current efficiency. Three electrons are required per iron atom for the overall Fe(III) – to – Fe reaction.
An important distinction is that the minimum reversible electrical work is not the same as the practical electricity consumption in a high-temperature MOE plant.
The essential distinction is between the theoretical electricity requirement, an engineering estimate for a future industrial plant, and the actual measured consumption of a commercial-scale MOE installation.
These are not interchangeable. Boston Metal’s technology has been developed through pilot-scale and scale-up activities, but a definitive, independently verified electricity-consumption figure in kWh per tonne of iron for a fully commercial MOE steel plant should not be assumed without published operating data.
For example, at approximately 1,600º C, a large amount of energy is also required to heat the feed, maintain the molten bath and compensate for heat losses. Electrical resistance can provide part of this heat internally, but it does not eliminate the need for an overall energy balance.
4.2. Specific electricity consumption: kWh per tonne of iron
The following Table (14,15,15bis,16,17), provide a useful engineering comparison. The first is a thermodynamic/engineering minimum; the second is a published estimate for MOE steelmaking; the third is experimental data from a different molten-oxide electrolysis system, not Boston Metal’s industrial cell.
|
Parameter |
Electricity consumption |
Status |
| Theoretical minimum for high-temperature MOE | Approxim 1,800 kWh/t Fe | Thermodynamic/engineering estimate under idealised conditions |
|
Published MOE steelmaking estimate |
13 GJ/t steel = 3,611 kWh/t steel |
Process-level estimate cited in a Columbia University steel-industry presentation |
|
Experimental iron electrolysis in a separate molten-oxide system |
2,600 kWh/t Fe reported for a process close to the thermodynamic minimum |
Research literature; not Boston Metal’s measured consumption |
|
Boston Metal industrial cell |
Not publicly quantified in the cited company announcement |
Industrial cell commissioned; tonnage-scale production reported, but no specific kWh/t figure supplied |
Important: the value of 3,611 kWh/t is a published process-level estimate, not a verified operating measurement from Boston Metal. Similarly, the 2,600 kWh/t figure should not be attributed directly to Boston Metal
4.3.- The Fundamental Difference MOE Compared with BF and H₂-DRI
This comparison is essential for understanding the future of MOE (4,8,9).
|
Charact |
Blast Furnace |
H₂-DRI + EAF |
MOE |
|
Reducing agent |
C/CO |
H₂ |
Electricity |
|
Reduction temperature |
~1,000–2,000 °C |
~600–1,000 °C |
>1,600 °C |
|
Initial product |
Liquid pig iron |
Solid DRI |
Liquid Fe |
|
Direct CO₂ |
Very high |
Very low o Cero with H2 |
Potentially zero |
|
H₂ required |
No |
Yes |
No |
|
Coke |
Yes |
No |
No |
|
EAF required |
Not necessarily |
Yes |
Not necessarily |
|
Pelletization |
Normally |
Normally |
Potentially reduced/eliminated |
|
Sintering |
Yes in BF |
Not necessarily |
Potentially not required |
|
Reducing gas |
Yes |
Yes |
No |
|
Electricity requirement |
Moderate |
Very high |
Very high |
|
High-grade ore required |
Not necessarily |
Important |
Potentially broad |
|
Maturity |
Commercial |
Commercial/ emerging |
Demonstration |
|
Scalability |
Very high |
High |
Under development |
The principal conceptual advantage of MOE is that it electrifies the metallurgical reaction directly, whereas H₂-DRI indirectly electrifies iron production through hydrogen generation.
4.4.- Potential advantages of MOE over BF and H2-DRI
Global steel production continues to depend primarily on coal-based routes. A scientific review published in npj Materials Sustainability (9) identifies iron electrolysis, including molten oxide electrolysis, among the routes with potential to produce low- or near-zero-emission iron and steel.
The advantage of MOE is that it attempts to eliminate several processes simultaneously.
Conventional Route
Ore → sinter/pellet → coke → blast furnace → pig iron → BOF → secondary metallurgy → steel
H₂-DRI Route:
Ore → pellet → H₂ → DRI → EAF → steel
Other routes
MOE Route:
Ore → MOE → liquid iron → secondary metallurgy → steel
Boston Metal states:
– That its process could eliminate in BF stages such as:
- coke making;
- sintering;
- pelletization;
- blast-furnace reduction;
- BOF conversion.
-Advantages over conventional DR, and H2 – DRI
It avoids the hydrogen-production stage and associated electrolyser capital investment.
It does not require hydrogen storage, compression or a reducing-gas recycle loop.
It can potentially produce liquid iron directly, avoiding the need to melt DRI in a separate furnace.
It offers a potential route to using a broader range of iron-bearing feedstocks, subject to impurity management and cell-specific feed requirements.
Modular cells may allow capacity to be increased by adding cells or electrode assemblies.
These are potential advantages, not guarantees of lower total cost.
In particular, MOE still requires substantial electricity, and the direct use of liquid iron does not eliminate the need for appropriate steel refining and casting equipment.
This simplification is probably the most important industrial argument in favor of MOE.
———–
Other advantage Compared with H₂-DRI: The Ore
One of the problems associated with H₂-DRI is the need for suitable raw materials.
The industry requires:
- high-quality pellets;
- high Fe content;
- low gangue levels;
- good reducibility;
- low impurity content.
SUSTAIN, for example, points to problems associated with the availability of suitable-quality ore and with the supply and price of green hydrogen
Boston Metal identifies one potential advantage of MOE precisely in this area: its process is intended to be compatible with a much broader range of ores.
If this claim is demonstrated at commercial scale, it could become an enormous strategic advantage.
5.- Industrial development and commercial status .
5.1.- The Decisive Breakthrough: Boston Metal
Boston Metal originated from research developed at MIT.
The company has developed MOE technology toward cells considerably larger than the original laboratory experiments. MIT explains that the technology evolved from experiments producing programs to installations capable of producing hundreds of kilograms and subsequently tonnes.
2013 — Scientific publication: Allanore, Yin and Sadoway published their research on chromium-based anodes in Nature (1).
2014 — Semi-industrial development: Boston Metal’s company history records commissioning of a semi-industrial MOE cell (10).
March 2025 — Boston Metal announced a very important milestone: An industrial MOE cell with multiple inert anodes began producing steel at tonnage scale (4, 5, 6).
This is very important because the question changes from: “Is it possible to produce iron by MOE?” to “Can we reliably and economically produce millions of tonnes per year?”
This is the core of the Bolton process’s viability at an industrial level.
2026 — Continued commercial development: The company reports further investment to scale its Critical Metals business and describes MOE Steel as a technology intended for subsequent deployment (10).
5.2.- The Real Situation of the Technology in 2026
Here we must be very careful.
I do not consider it correct to state that MOE Steel is already commercially available on a large scale.
Because: several questions remain essential for commercial assessment.
Can the cell operate reliably over prolonged campaigns?
What are the actual electricity consumption and current efficiency at sustained industrial production rates?
How frequently must anodes and refractory components be replaced?
Can the cell handle variable ore compositions while consistently producing iron that meets downstream requirements?
What are the maintenance costs, production availability and total capital costs per tonne of annual capacity?
Can multiple cells operate reliably as part of an integrated steelworks?
Public announcements of successful cell commissioning do not, by themselves, answer all these questions.
Boston Metal’s stated business model is to license its MOE platform to steel producers and supply metallic inert anodes, rather than to become a conventional steel producer itself. Its commercial strategy and future demonstration plans should be distinguished from an established fleet of commercial-scale MOE steel plants (10).
The OECD placed molten oxide electrolysis at a still relatively low technology readiness level, compared with mature steelmaking technologies. The same assessment indicates that MOE has significant emissions-reduction potential but still needs to overcome important industrialization barriers.
Therefore:
2026
Laboratory → Pilot → Industrial Demonstration
but not yet:
Demonstration → Mass Steel Production
5.3.- . News Item That Must Be Correctly Interpreted (2026).
There is a particularly important aspect.
In May 2026 Boston Metal announced an additional investment of $75 million, bringing the total capital raised to more than $500 million.
However, the company explained that the immediate objective of this financing was to accelerate the commercial deployment of MOE Critical Metals, particularly:
- niobium;
- tantalum;
- vanadium;
- nickel;
Including production from low-grade feedstocks and industrial waste.
This means that Boston Metal is initially using the potential of MOE where the economics may be more favorable.
It means that the company is using a staged commercialization strategy:
Stage 1
MOE → Critical metals
Stage 2
MOE → Ferroalloys / metallurgical applications
Stage 3
MOE → Iron
Stage 4
MOE → Mass steel production
This appears to be a very reasonable business strategy.
6.-. Main technical challenges and engineering risks.
6.1.- Anode durability and corrosion
The inert anode is arguably the most critical materials challenge. It must conduct electricity and evolve oxygen while resisting dissolution, oxidation and structural degradation in a corrosive molten oxide environment.
Anode degradation can lead to:
Increased operating costs and unplanned shutdowns.
Contamination of the iron or electrolyte by anode constituents.
Changes in cell voltage and current distribution.
Difficulties in maintaining consistent product quality.
Long-duration testing, corrosion analysis and reliable replacement procedures are therefore essential to the commercial development of MOE. The 2013 Nature study established a promising materials approach, but industrial service life must be assessed under representative operating conditions .
Scientific research conducted at MIT makes it possible to identify relevant materials.
Chromium-based alloys: research published in Nature demonstrated that chromium alloys, in molten oxide baths (such as MgO-CaO-SiO2-Al2O3), can develop a protective layer of chromium and aluminum oxides with a corundum-type structure (Cr2-ₓ AlₓO3) (1,19) a form of «dynamic self protection» which limits the consumption of the anode.
Iridium (Ir): used in laboratory experiments due to its resistance under specific conditions. It has been evaluated as an initial noble anode in molten oxide baths (such as MgO-CaO-SiO2-Al2O3) operating at temperatures above 1,538 °C. Its stability depends largely on the basicity of the electrolyte (showing a lower wear rate in acidic slags with high silica content compared to basic slags); however, its high cost limits its large-scale commercial viability (20, 21).
The most solid reference point for explaining Boston Metal’s industrial concept is a proprietary, inert metal alloy.
6.2.- Electrolyte composition and control
The electrolyte must, first dissolve or accommodate iron oxide, second conduct ionic current and remain stable at operating temperature. Its composition also affects viscosity, electrical conductivity, oxygen-ion transport and corrosion of the cell lining.
A viable industrial electrolyte must balance competing requirements:
High electrical conductivity to reduce resistive losses.
Suitable solubility and transport of iron-bearing species.
Chemical compatibility with the electrodes and refractory lining.
Low contamination of the iron product.
Stable operation as ore and slag composition change.
Experimental studies show that the multiple oxidation states of iron and the chemistry of the molten oxide phase complicate the reduction process.
So the process as a whole is extraordinarily complex.
The exact industrial electrolyte formulation used in Boston Metal’s commercial-scale MOE steel cells has not been fully disclosed publicly. Therefore, the following table describes the general chemistry of molten oxide electrolysis rather than claiming a verified proprietary recipe.
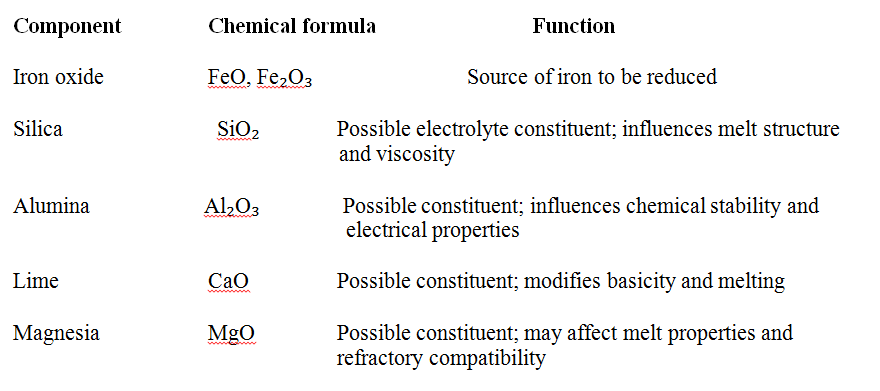
Boston Metal’s published patent literature describes supporting electrolytes containing combinations of metal oxides, including the following candidates (8, 22, 10, 23) :
Cerium oxide — CeO2
Lanthanum oxide — La2O3
Strontium oxide — SrO
Barium oxide — BaO
Beryllium oxide — BeO
Magnesium oxide — MgO
Calcium oxide — CaO
These are patent-disclosed candidate constituents, not a confirmed recipe for the current MOE Steel cell. The patent describes alternative compositions, rather than requiring all these oxides in one electrolyte.
6.3.- Refractory and thermal management
The cell operates at extreme temperature, with molten metal and an aggressive oxide electrolyte in contact with its internal materials. Refractory selection must account for chemical attack, thermal shock, electrical properties and possible contamination.
Thermal management is equally important. Excessive heat loss increases electricity consumption, while insufficient heat input can cause freezing or solidification of the bath. A commercial design must maintain the necessary temperature distribution without creating damaging hot spots.
In Resume Thermal Balance and Joule Heating
The MOE process is self-heating via Joule heating. As massive electrical currents pass from the inert anodes through the liquid electrolyte to the cathode, the inherent electrical resistance of the fluid generates the thermal energy needed to maintain 1,600°C (24).
If the cell receives too much power, the protective freeze lining can melt away, exposing the brick to catastrophic corrosion and causing containment failures. Conversely, if the cell cools too much, the entire block of electrolyte can solidify, resulting in a catastrophic «cell freeze» that permanently ruins the module (25).
Direct Comparison: MOE vs. Traditional Refractory Systems
|
Parameter |
Traditional Steel Refractories (Blast Furnace/EAF) |
MOE Cell Refractories |
| Primary Containment |
Sacrificial refractory bricks (Mag-Carbon, Alumina) |
Stable Freeze Lining (solidified electrolyte) |
|
Thermal Strategy |
Minimize heat loss entirely to conserve fossil energy |
Controlled heat flux to maintain the frozen boundary layer |
|
Heating Source |
Combustion of coke/coal or plasma arcs |
Internal Joule heating from bulk electrical current |
|
Risk Profile |
Gradual brick thinning and chemical erosion |
Sudden shell leaks if the freeze lining melt |
6.4.- Feedstock impurities and steel quality
Boston Metal presents MOE as a technology with the potential to use a broad range of iron ores. However, the claim that all ore grades can be used should be interpreted as a development objective rather than as proof that every ore is economically suitable without preparation.
Gangue minerals and other impurities may accumulate in the electrolyte, alter its chemistry or affect the final metal. The industrial process will need appropriate feed characterization, electrolyte management and downstream refining.
6.5.- Electrical infrastructure and plant integration
MOE requires a reliable high-current DC supply, robust electrical connections and effective control systems. The plant must also integrate ore handling, liquid-iron tapping, oxygen management, maintenance access and downstream steelmaking (see Fig nº1).
Where electricity is supplied by a nuclear plant, renewable generation or a combination of sources, the design must account for availability, load-following requirements, backup supply and the cost of connecting the electrochemical plant to the electricity system.
6.6.-. MOE has an Enormous Electricity Requirement
Here we encounter its main disadvantage compared with H₂-DRI.
MOE replaces chemical energy with electrical energy.
The electricity required is not only that associated with the electrochemical reaction. The following must also be considered:
- bath heating;
- electrical losses;
- thermal losses;
- melting;
- temperature maintenance;
- ore feeding;
- metal extraction;
- auxiliaries;
- transformers;
- rectifiers.
Therefore, the availability of abundant and inexpensive electricity will be decisive (Nuclear Power) (12).
MIT has indicated that MOE requires an almost carbon-free electricity source in order to maximize its environmental advantages.
As indication (26):
|
Parameter |
Electricity consumption |
Status |
|
Theoretical minimum for high-temperature MOE |
Approximately 1,800 kWh/t Fe |
Thermodynamic/engineering estimate under idealised conditions |
|
Published MOE steelmaking estimate |
13 GJ/t steel = 3,611 kWh/t steel |
Process-level estimate cited in a Columbia University steel-industry presentation |
|
Experimental iron electrolysis in a separate molten-oxide system |
2,600 kWh/t Fe reported for a process close to the thermodynamic minimum |
Research literature; not Boston Metal’s measured consumption |
|
Boston Metal industrial cell |
Not publicly quantified in the cited company announcement |
Industrial cell commissioned; tonnage-scale production reported, but no specific kWh/t figure supplied |
Important: the value of 3,611 kWh/t is a published process-level estimate, not a verified operating measurement from Boston Metal. Similarly, the 2,600 kWh/t figure should not be attributed directly to Boston Metal.
6.6.1.- MOE + Renewables
A future configuration could be:
Wind + Solar + Hydropower  Electrical grid / storage
Subestacion Secondary Rectifier MOE Liquid Iron
Metallurgy (ladle) Continous castingRolling.
6.6.2.- MOE + Nuclear Energy: A Particularly Interesting Combination (10)
For the study being developed on nuclear energy + hydrogen + steelmaking, MOE introduces an additional and very interesting possibility:
Nuclear reactor electricity MOE liquid iron
Secondary Metallurgy Continous casting Rolling.
In this case, hydrogen production is not required.
A nuclear reactor could provide:
- electricity 24h / 7days;
- firm power;
- high availability;
- grid stability;
- reduced dependence on electrical storage.
This could be particularly attractive for MOE because the cell operates at extremely high temperature and requires a continuous and stable electrical supply.
Conceptually:
H₂-DRI
Nuclear → electricity → H₂ → DRI……..
whereas:
MOE
Nuclear → electricity → MOE → liquid Fe
This makes MOE a technology that deserves to be included in any serious study of nuclear energy + green steel (12).
7.- Extraordinary Advantage: No Hydrogen Required
This point is extremely important for the future.
H₂-DRI requires:
Renewable electricity → electrolyzer → H₂ → compression → storage → DRI reactor → EAF
MOE requires:
Electricity → MOE → liquid iron
Therefore, MOE could avoid:
- electrolyzers;
- H₂ compressors;
- H₂ storage;
- H₂ pipelines;
- reducing-gas recirculation;
- H₂/H₂O control;
- reducing-gas heating.
This could simplify the plant enormously.